HOSE

Engineered textile hoses provide reliable air guidance and material transport in demanding industrial and mining environments. Antistatic and flame-retardant materials help ensure safe operation under challenging conditions and continuous use.

Why Are Technical Textile Hoses Used in Industrial and Mining Applications?

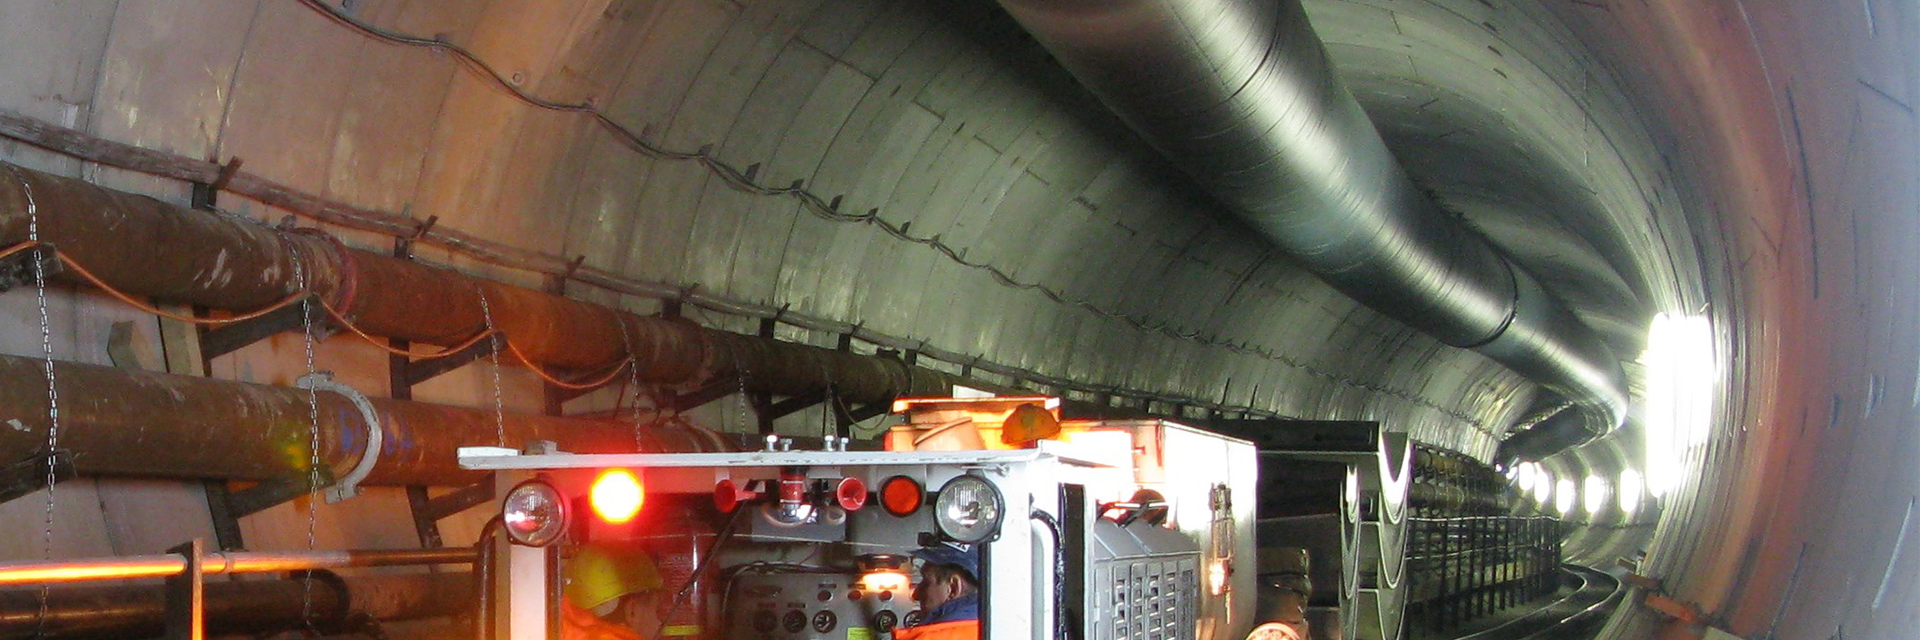
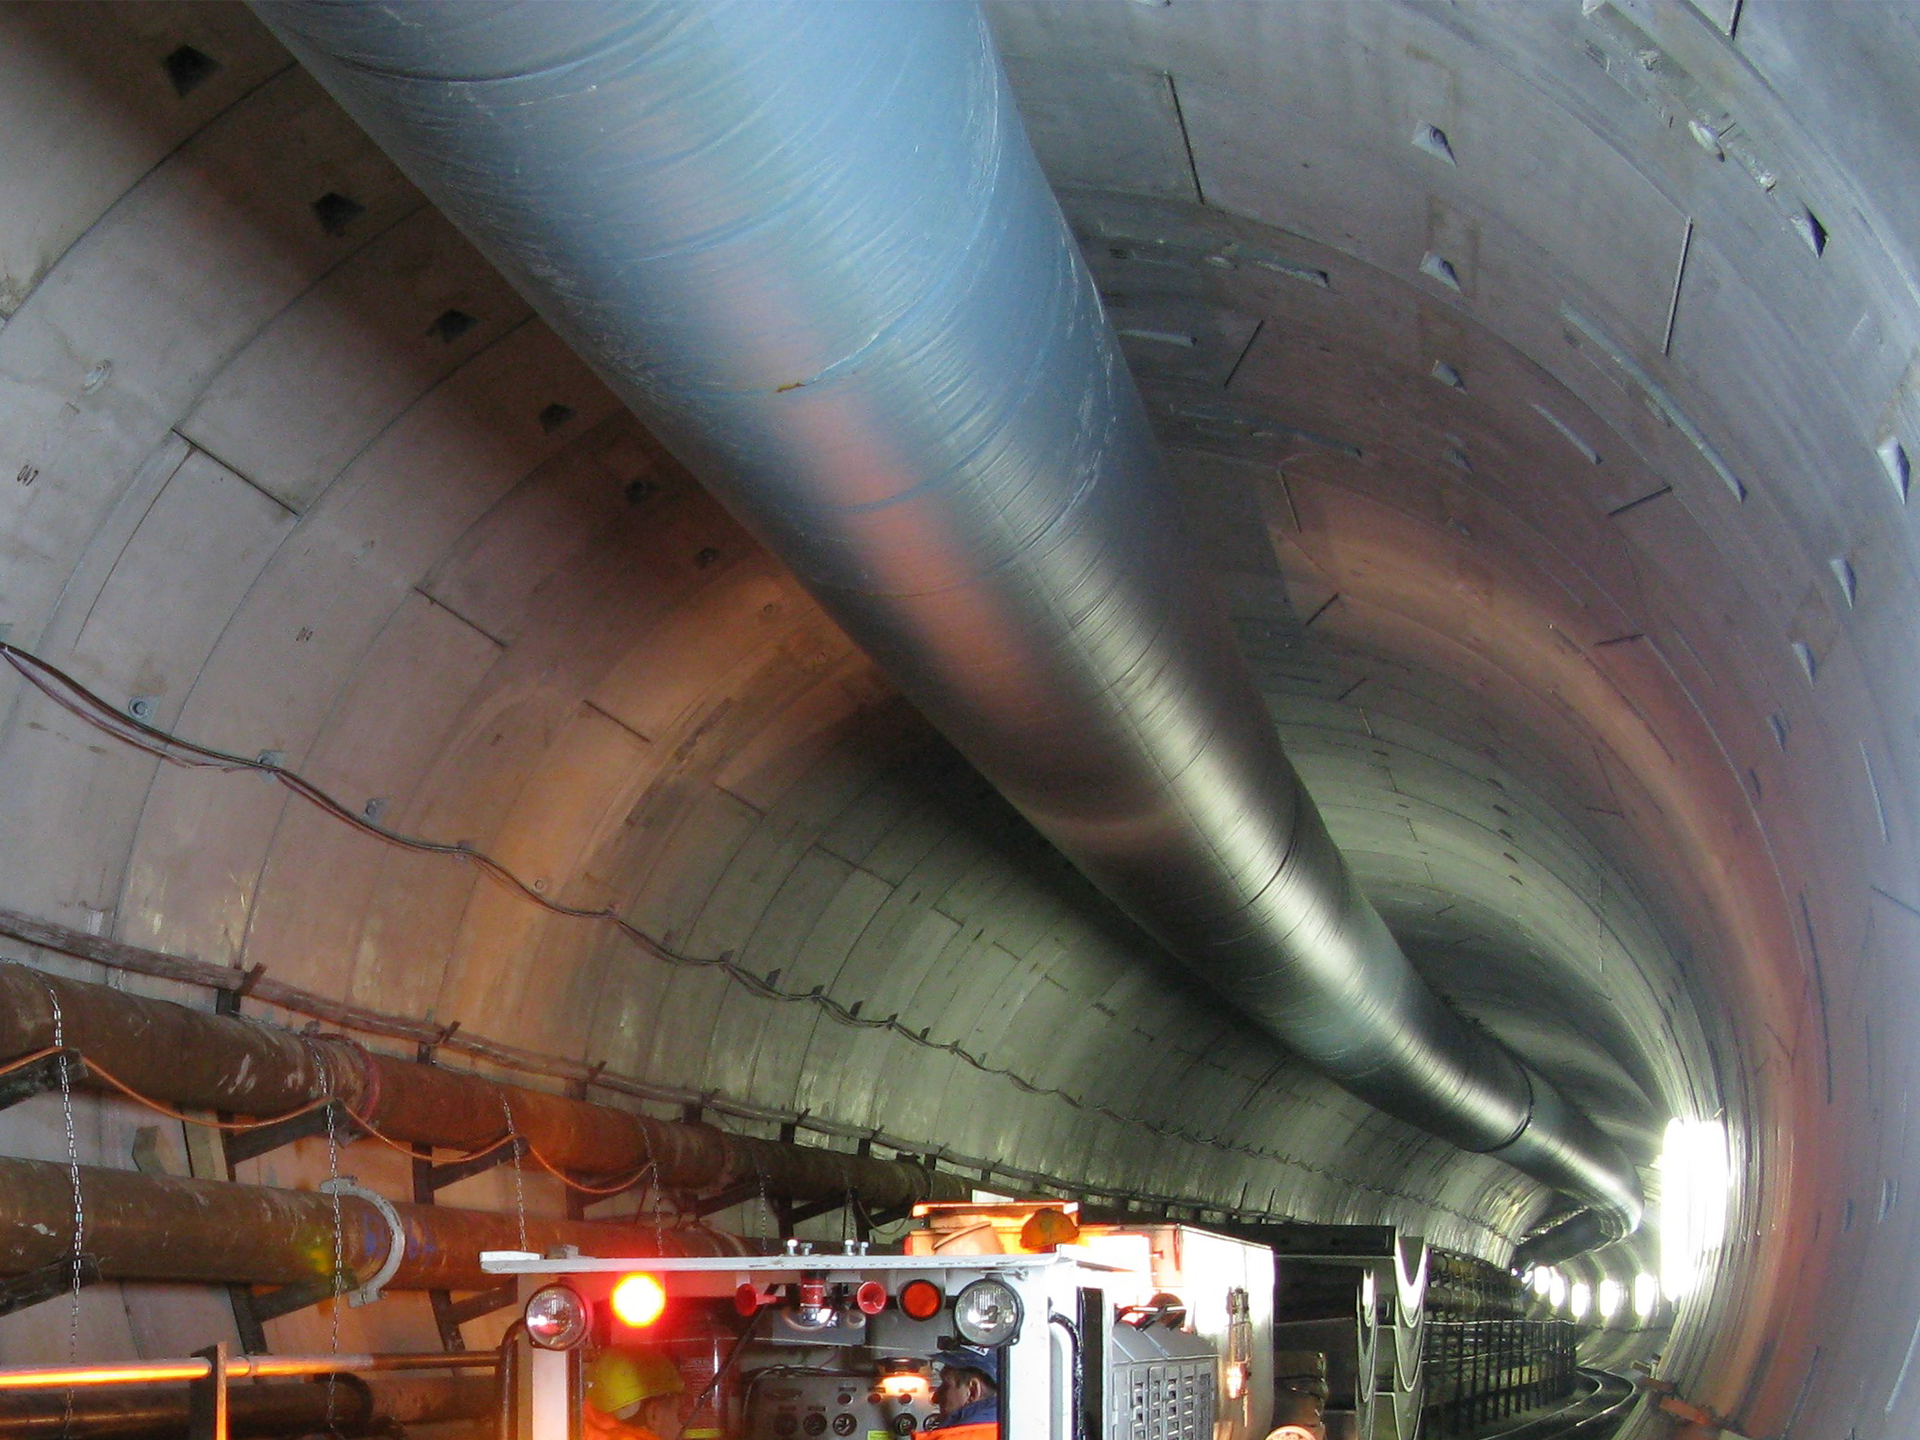
Technical textile hoses are used to transport air, dust, particles and other media in environments where flexibility, durability and safety are critical. In mining operations, ventilation systems rely on hose materials that withstand mechanical stress while maintaining dimensional stability during continuous operation. Industrial hose systems must also comply with specific safety requirements, including antistatic properties and flame-retardant performance. Selecting the appropriate hose material helps improve operational reliability, supports system efficiency and reduces maintenance requirements in demanding working conditions.
  • Antistatic Protection

    Supports safe operation in environments where electrostatic discharge must be controlled.
  • Flame-Retardant Design

    Helps meet safety requirements in industrial and underground applications.
  • High Flexibility

    Allows easy installation and handling in confined or complex layouts.
  • Durable Construction

    Designed to withstand demanding operational conditions and mechanical loads.
  • Reliable Airflow

    Supports consistent air transport and ventilation performance.
  • Industrial Compliance

    Suitable for applications requiring specific technical and safety standards.

Fields of Applications

Technical textile hose materials are used in a variety of industrial air handling and transport systems, including:
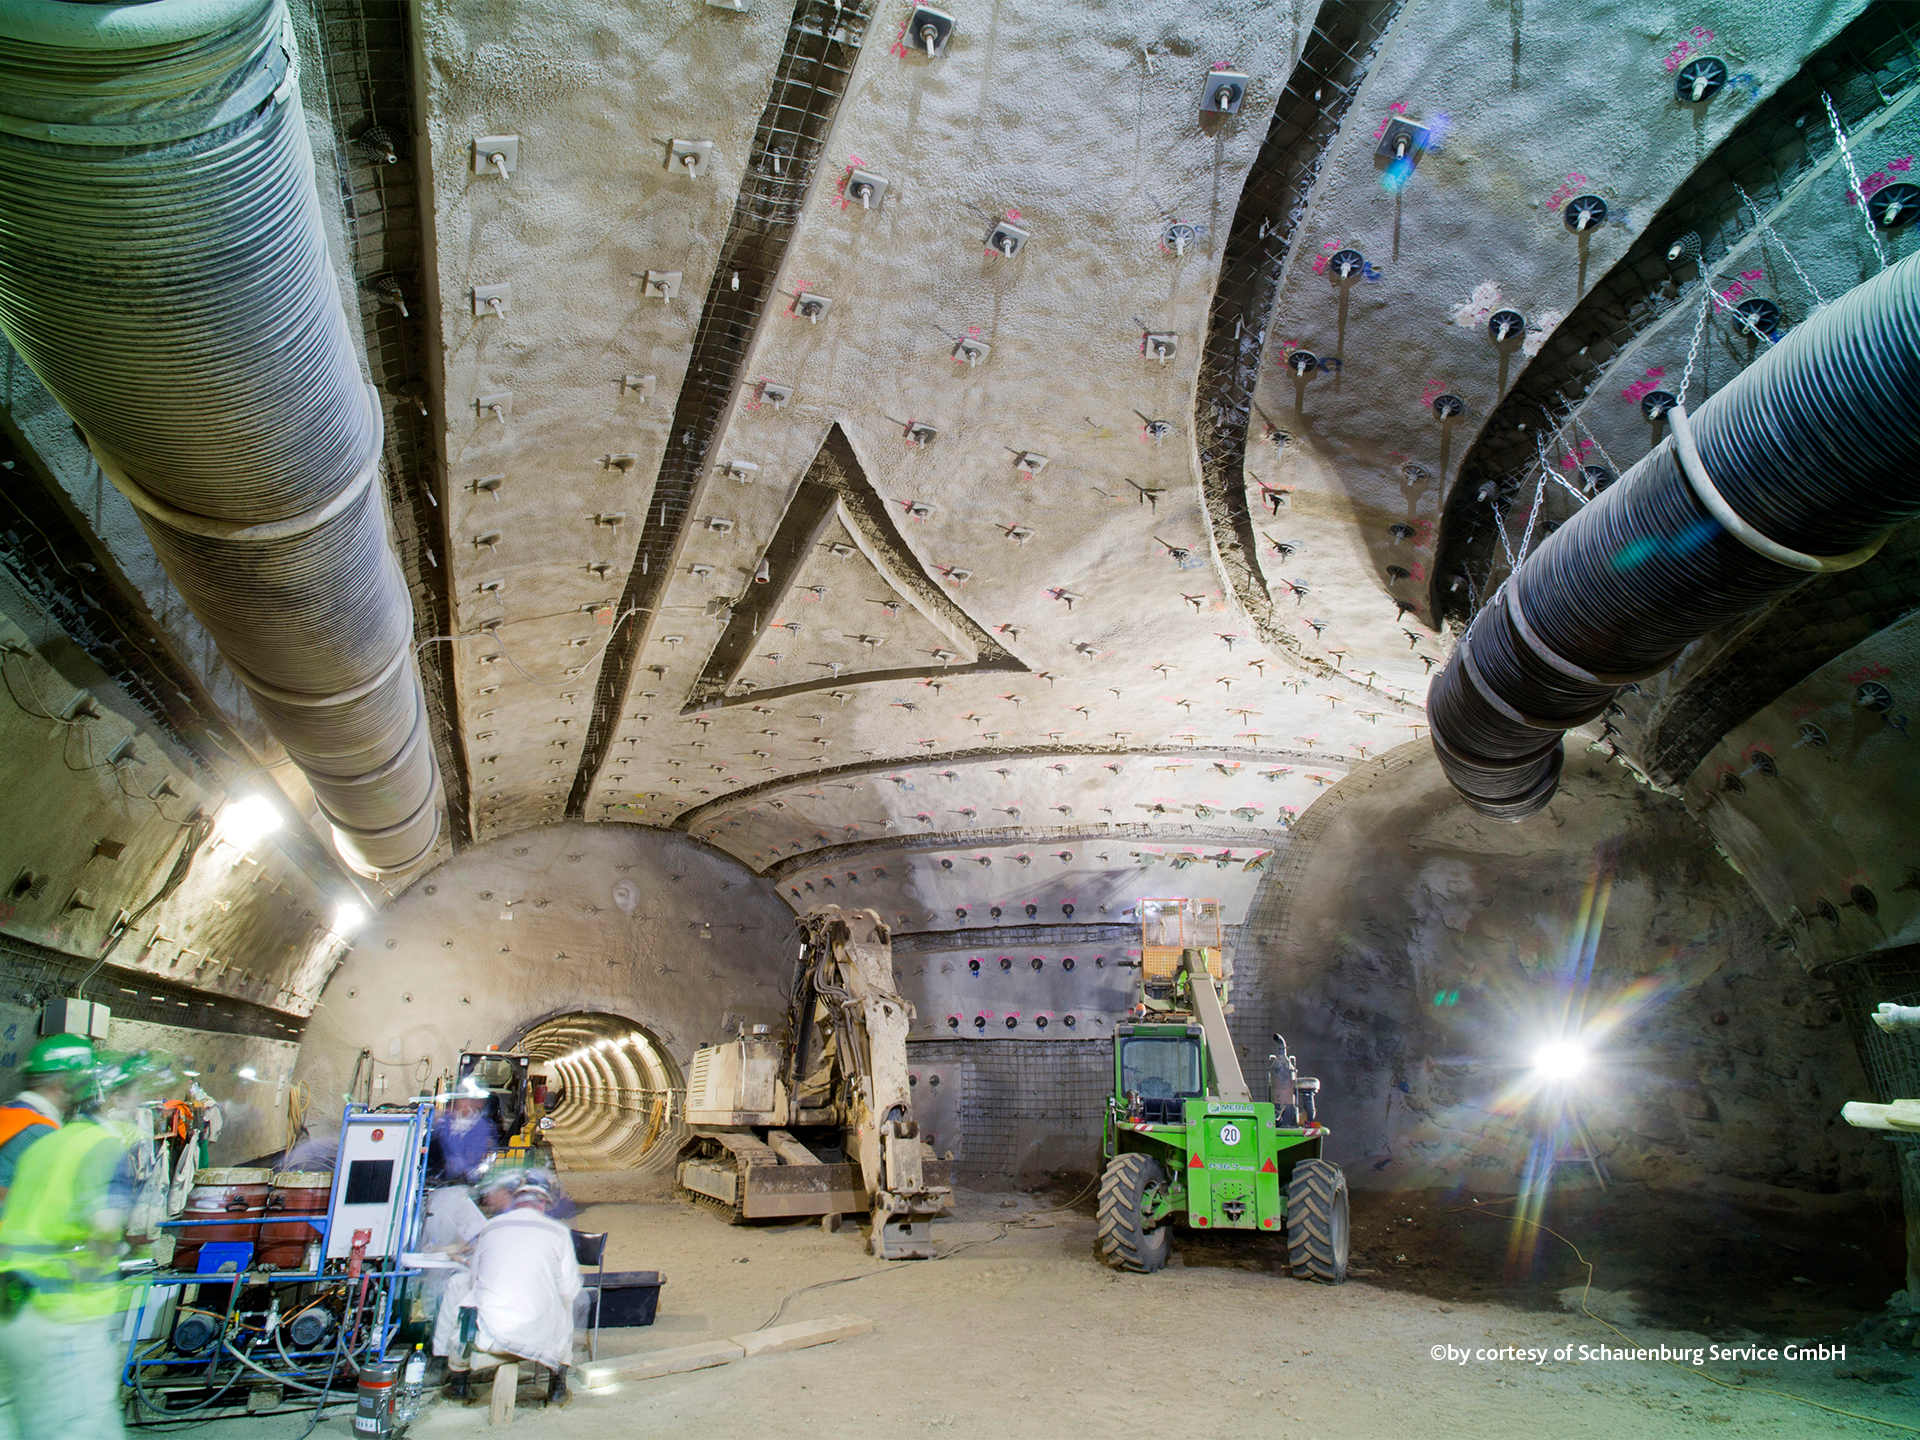
 

  • Mining ventilation systems
  • Underground air distribution networks
  • Dust extraction systems
  • Industrial material transport hoses
  • Temporary ventilation installations
  • Tunnel construction projects
  • Process air management systems


Properties

Hose materials for industrial applications are designed to provide the following performance characteristics:


  • Antistatic material properties
  • Flame-retardant performance
  • Good mechanical strength
  • Flexible handling and installation
  • Reliable dimensional stability
  • Resistance to demanding operating conditions
  • Suitability for continuous industrial use

Hose Materials for Industrial Ventilation and Air Transport


Our hose portfolio includes technical textile materials designed for ventilation, air transport and mining applications. Products are developed to meet demanding operational requirements, including antistatic performance and compliance with relevant industry standards.

Q&A - Hose Membranes


Looking for the right membrane for your Hose project?

Our experts support you in selecting coated textile solutions for mining ventilation, industrial airflow management and specialized hose applications.